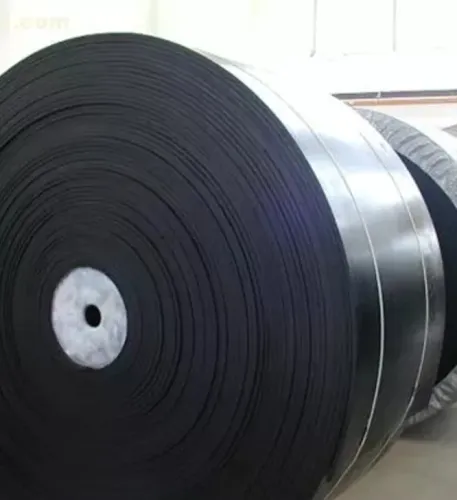

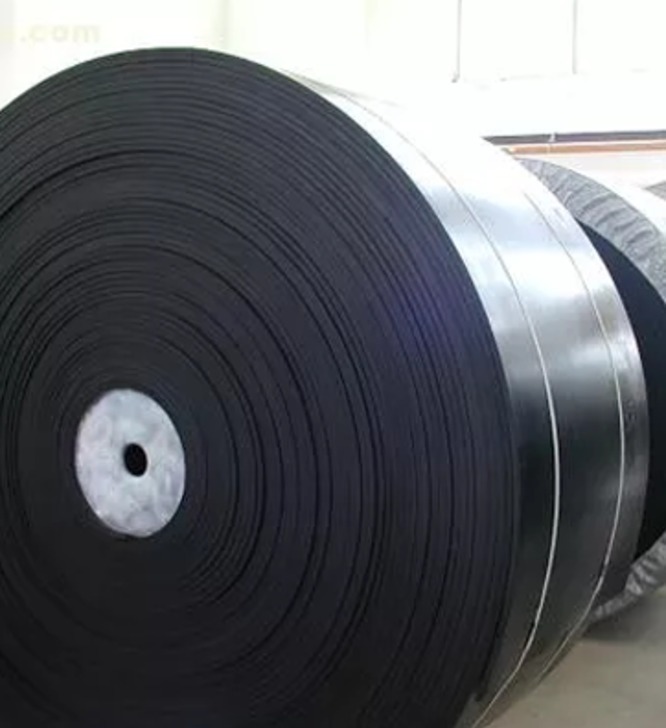
Heavy industries operate in some of the most demanding environments. From mining and steel processing to cement manufacturing, power generation, and large-scale material handling, conveyor belts are expected to transport massive loads continuously under harsh operating conditions. Choosing the best conveyor belts for heavy industries requires careful consideration of performance, durability, and application requirements.
Unlike general-purpose conveyor systems, heavy industrial applications expose conveyor belts to abrasion, impact, moisture, chemicals, sharp materials, and high temperatures. Standard belts often deteriorate quickly when subjected to these conditions, resulting in frequent replacements and costly production interruptions.
The ideal heavy-duty conveyor belt combines strong reinforcement with specially formulated rubber compounds that resist wear and maintain structural integrity over extended periods. High tensile strength helps the belt carry heavy loads without excessive stretching, while abrasion-resistant surfaces reduce material loss caused by constant friction.
Heat resistance is another essential characteristic in industries such as cement manufacturing, foundries, and metal processing. Conveyor belts designed for elevated temperatures help maintain operational stability while reducing the risk of premature material degradation.
For mining applications, conveyor belts must withstand continuous impact from rocks, ores, and other abrasive materials. Reinforced construction and high-quality rubber compounds contribute to improved durability in these demanding environments.
Proper conveyor belt selection also depends on operational factors such as conveyor length, belt speed, load weight, incline angle, and environmental conditions. Evaluating these factors during the planning stage helps businesses choose a solution that supports reliable performance while minimizing maintenance requirements.
Regular inspections and preventive maintenance further contribute to conveyor belt longevity. Monitoring belt alignment, tension, pulley condition, and surface wear allows maintenance teams to identify potential concerns before they develop into costly failures.
Businesses increasingly recognize that investing in quality conveyor belts is an investment in operational continuity. Although premium products may involve higher initial costs, they often reduce maintenance expenses, minimize downtime, and improve long-term productivity.
Elcon Elastomers Pvt Ltd manufactures conveyor belts that serve diverse industrial sectors requiring dependable material handling solutions. By combining manufacturing expertise with quality materials and application-focused engineering, the company supports customers looking for conveyor systems capable of meeting demanding operational requirements.
For industries operating in challenging environments across Pune and beyond, selecting the right conveyor belt can significantly influence efficiency, equipment reliability, and long-term operational performance. Choosing a trusted manufacturing partner helps ensure that every conveyor solution is designed to support consistent productivity while meeting the practical demands of modern industry.